Project Overview
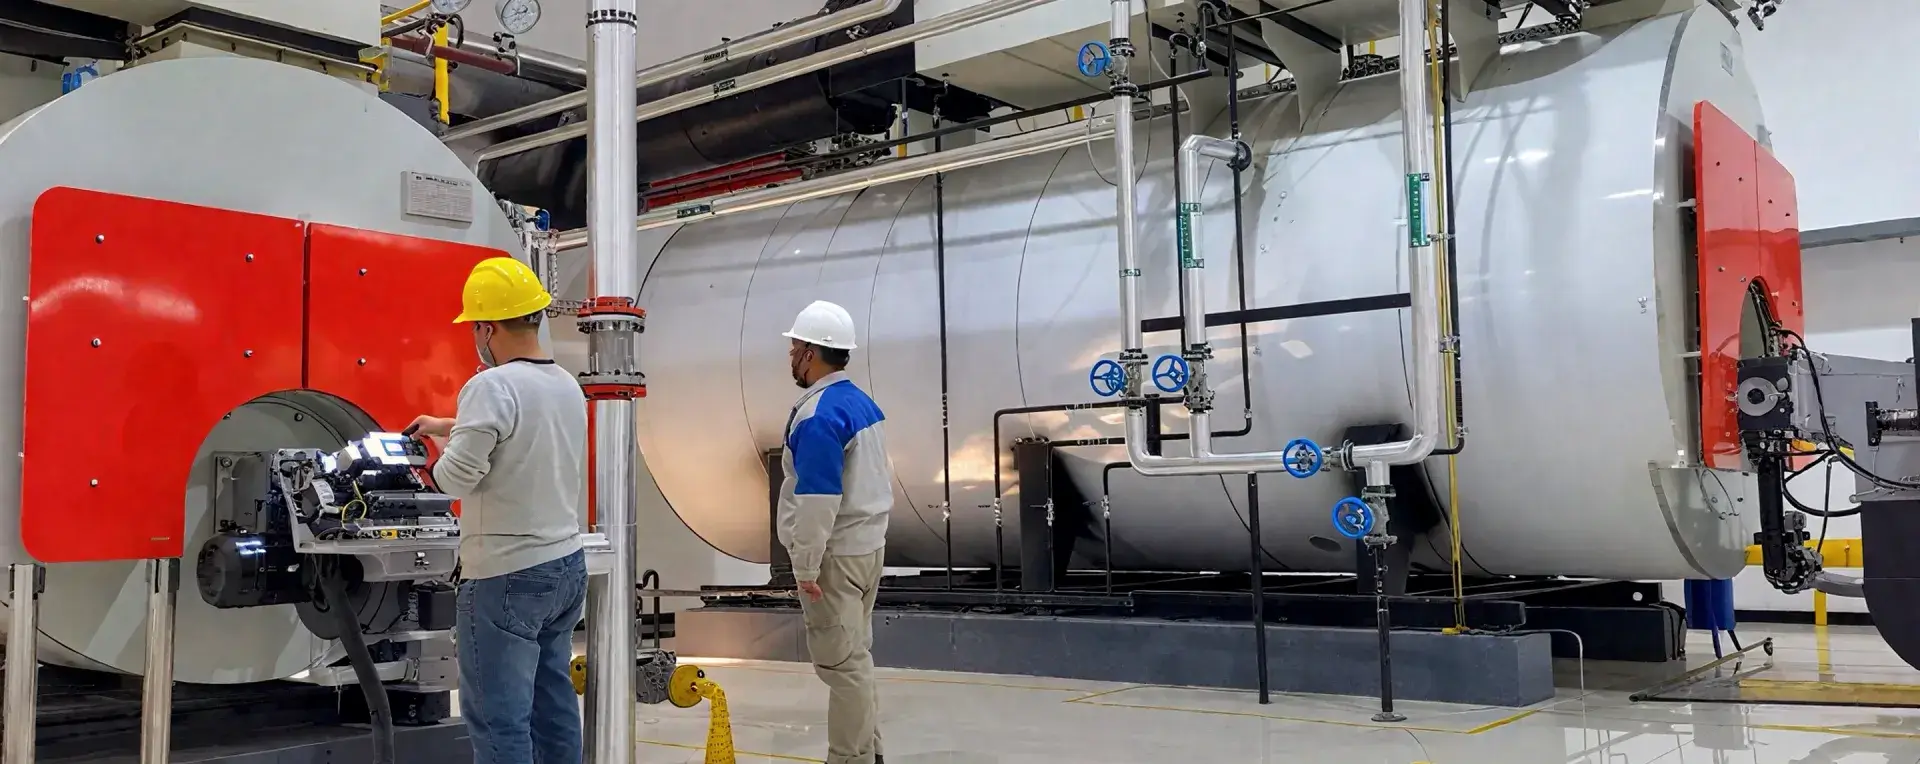
This food group is a well-known Thai meat processing and canned food export company, with products exported to markets in Southeast Asia, the Middle East, and Europe. Its production facilities require a large and stable supply of steam daily for core processes such as high-temperature sterilization and steaming. As environmental emission standards in Thai industrial zones have become increasingly stringent, the plant’s existing old boilers not only had low thermal efficiency and high energy consumption but also failed to meet the new regulations regarding nitrogen oxide emissions, creating an urgent need to install two new steam boilers.
After thoroughly evaluating the technical solutions, actual energy consumption data, and industry reputations of multiple international boiler brands, the food group ultimately selected the low-nitrogen once-through steam boiler solution provided by Huano Boilers, purchasing two units in a single transaction to completely replace the existing outdated equipment.
Solution
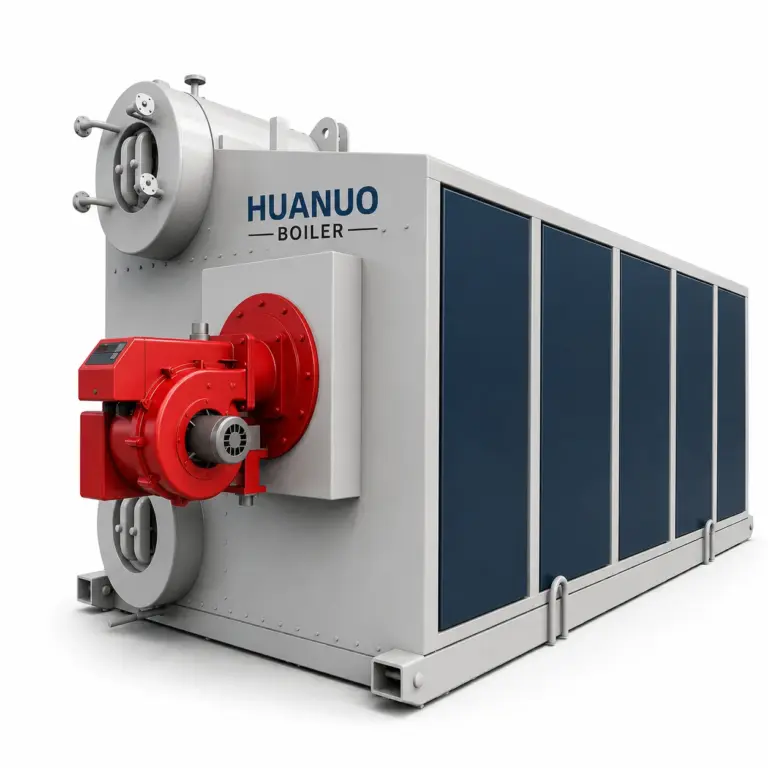
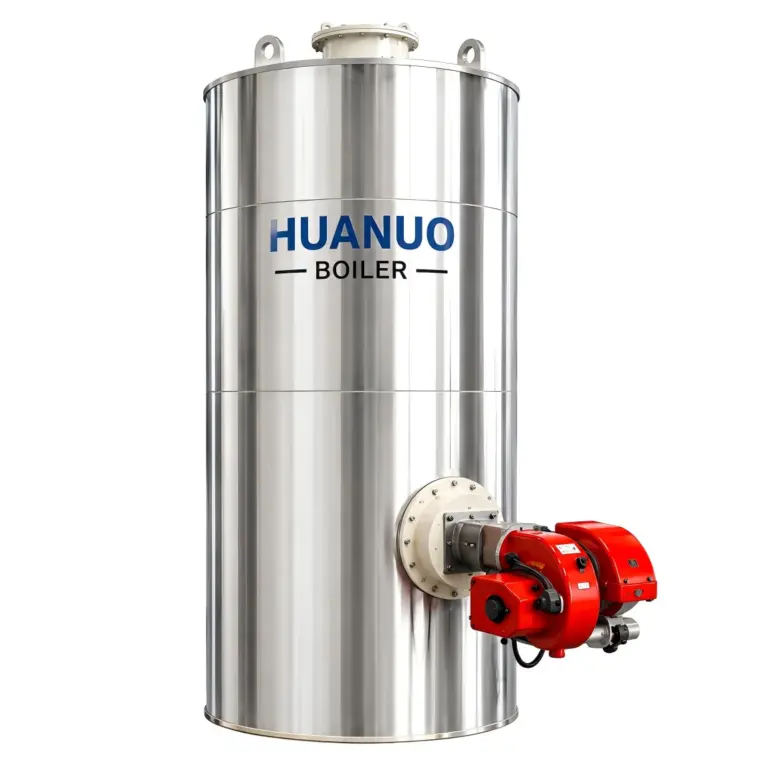
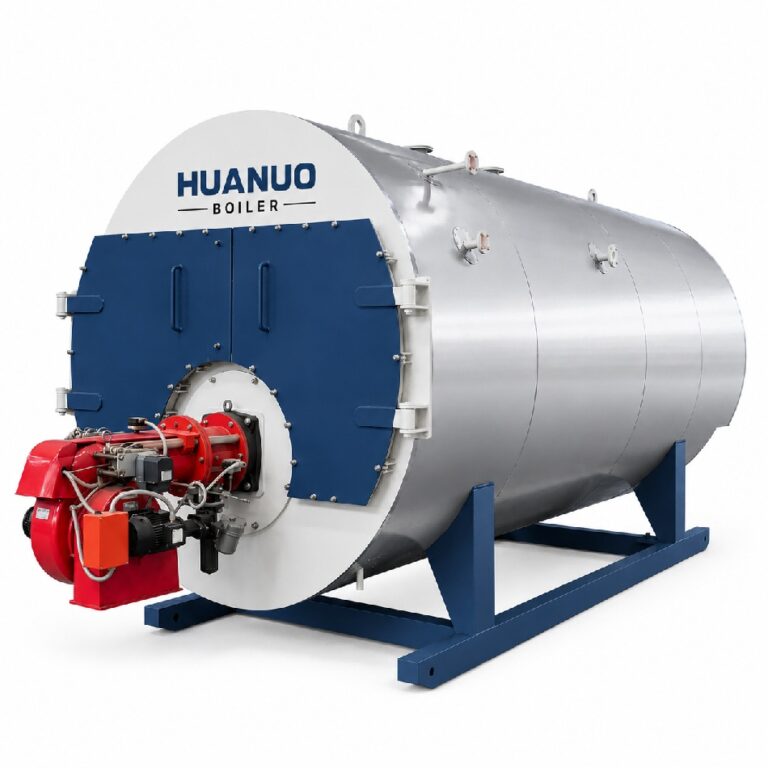
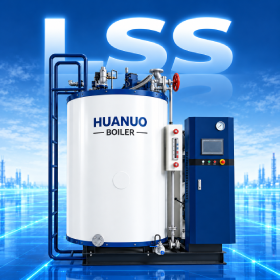
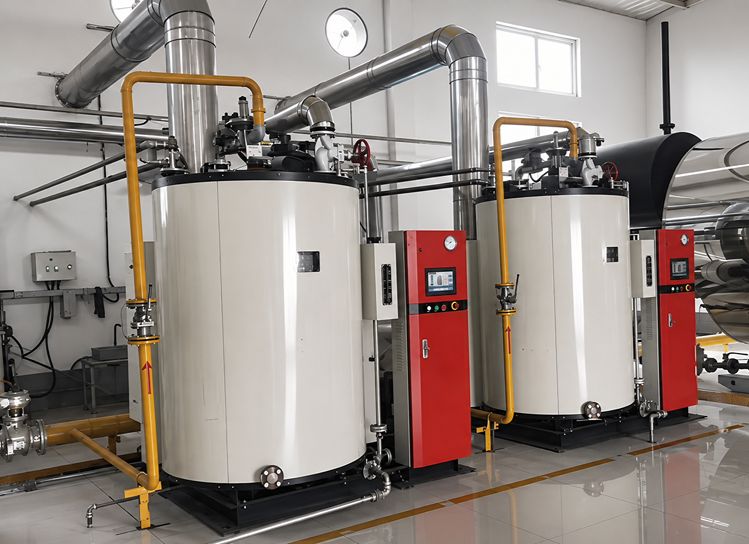
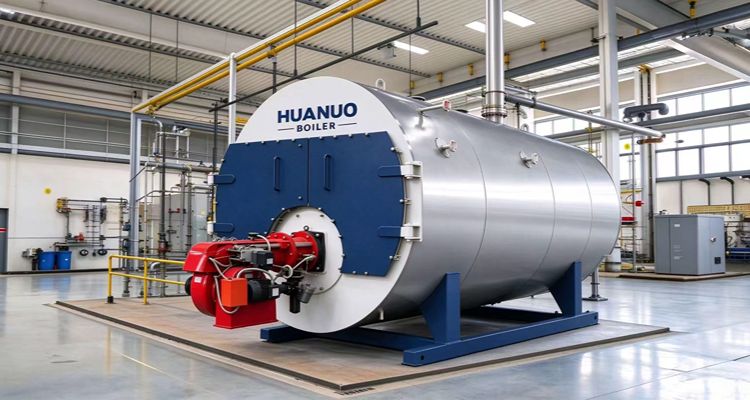
Addressing the characteristics of food production facilities—frequent start-ups and shutdowns, significant fluctuations in steam demand, and limited space—Huanuo Boilers configured two vertical LSS2.0-1.0-Q low-nitrogen once-through steam boilers for the client:
Request a Solution
The boiler body features a through-flow design comprising an upper header, a lower header, and water tubes, complemented by a high-efficiency steam-water separator, a water pump, and a low-nitrogen burner. Through precise calculations and optimized layout by Huanuo engineers, the equipment’s footprint was significantly reduced while ensuring rated output, freeing up valuable production space in the workshop and reducing infrastructure investment costs.
It takes only 2–4 minutes to go from a cold start to producing qualified steam, and just 20 minutes to reach full load from a cold state—perfectly suited for the frequent start-stop requirements of processes such as sterilization and steaming. The steam pressure is stable and the quality is dry saturated, significantly improving the uniformity of the sterilization process.
Equipped with fully automatic low-NOx combustion technology, NOx emissions are consistently controlled below 30 mg/m³—far exceeding local environmental regulations—ensuring immediate compliance with environmental inspections and completely eliminating the hassle of excessive emissions.
The control system supports fully automatic operation and load matching. The user interface is simple and intuitive, allowing local staff to operate the system proficiently after only a short training period, significantly reducing the workload associated with manual management.
Core Project Advantages
Comprehensive steam energy consumption is reduced by 20%, allowing for recovery of most of the investment in equipment upgrades within six months and a significant reduction in energy costs.
Steam supply is rapid and of consistent quality, resulting in superior product sterilization and a steady improvement in batch pass rates.
Emissions testing consistently meets compliance standards, enabling the company to successfully pass multiple international clients’ green audits and earn a reputation for green manufacturing.
The compact design requires minimal floor space, eliminating the need to expand the boiler room and saving on additional construction costs and installation time.
Client Testimonial

Somchai P.
Director of Production and Operations

Budi Santoso.
Equipment Manager, a major paper group in Indonesia

María González.
Production Director, a pharmaceutical company in Mexico

Ahmed Hassan.
Head of Engineering, a hotel group in Egypt

Mehmet Yılmaz
Production Manager, a textile dyeing and finishing company in Türkiye

Rafiq Islam.
Operations Supervisor, a garment washing company in Bangladesh

Khalid Al-Farsi
Plant Manager, a food processing plant in Saudi Arabia

Johan van der Merwe
Energy Manager, a beverage producer in South Africa

Rajesh Kumar
Technical Director, a chemical company in India

Dmitry Ivanov
Operations Manager, a district heating company in Russia

Camila Rojas.
Production Head, a fruit and vegetable processor in Chile