Project Overview
As a leading manufacturer of industrial chemicals in Indonesia, the company’s products are widely used in the textile, dyeing, and water treatment industries across Southeast Asia. As the Indonesian government continues to tighten emission standards for industrial air pollutants and implement incentives for green industries, the company’s aging boilers could no longer meet both energy efficiency and environmental protection requirements, creating an urgent need to upgrade to a high-efficiency, clean, and extremely stable steam supply system.
After a comprehensive comparison of technical proposals, measured energy efficiency, and proven track records in the chemical industry from multiple international boiler brands, the company ultimately selected the SZS series integrated condensing gas-fired steam boiler solution provided by Huanuo Boilers.
Solution
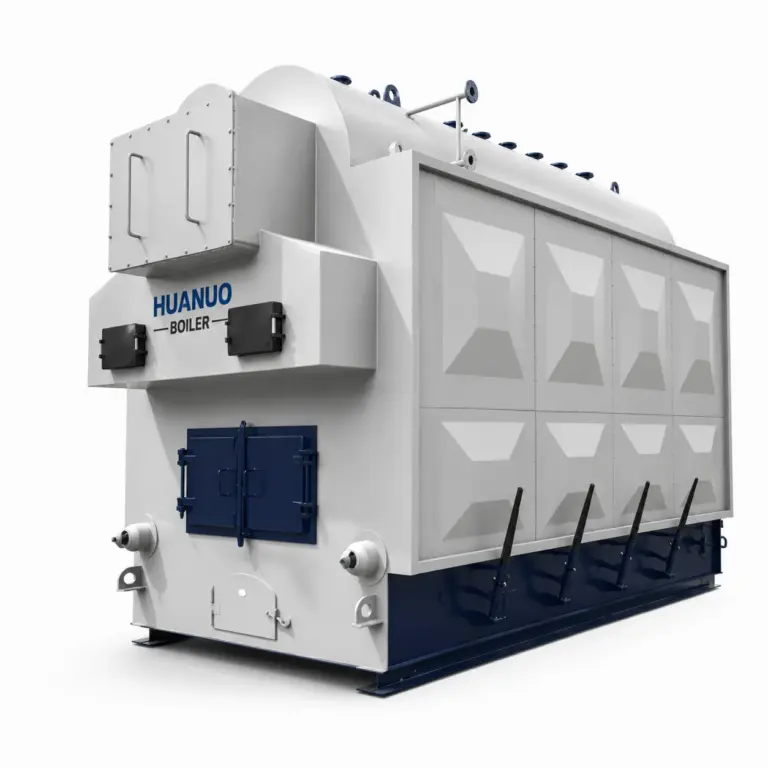
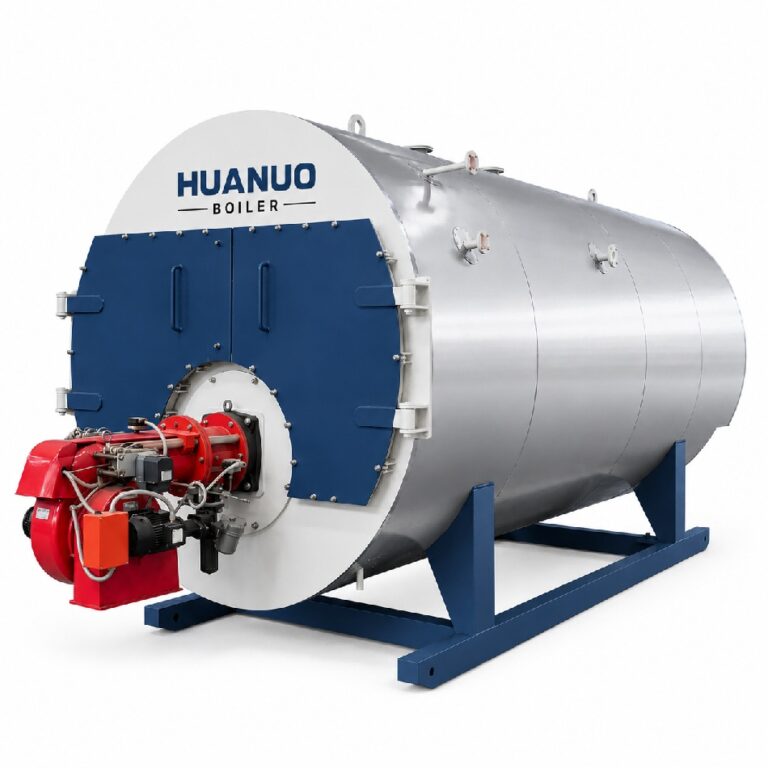
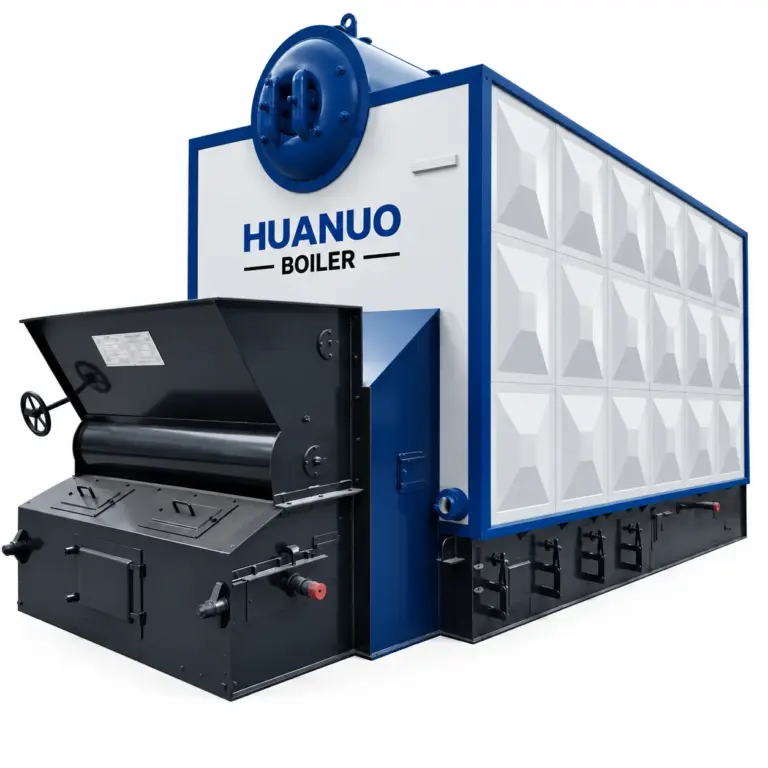
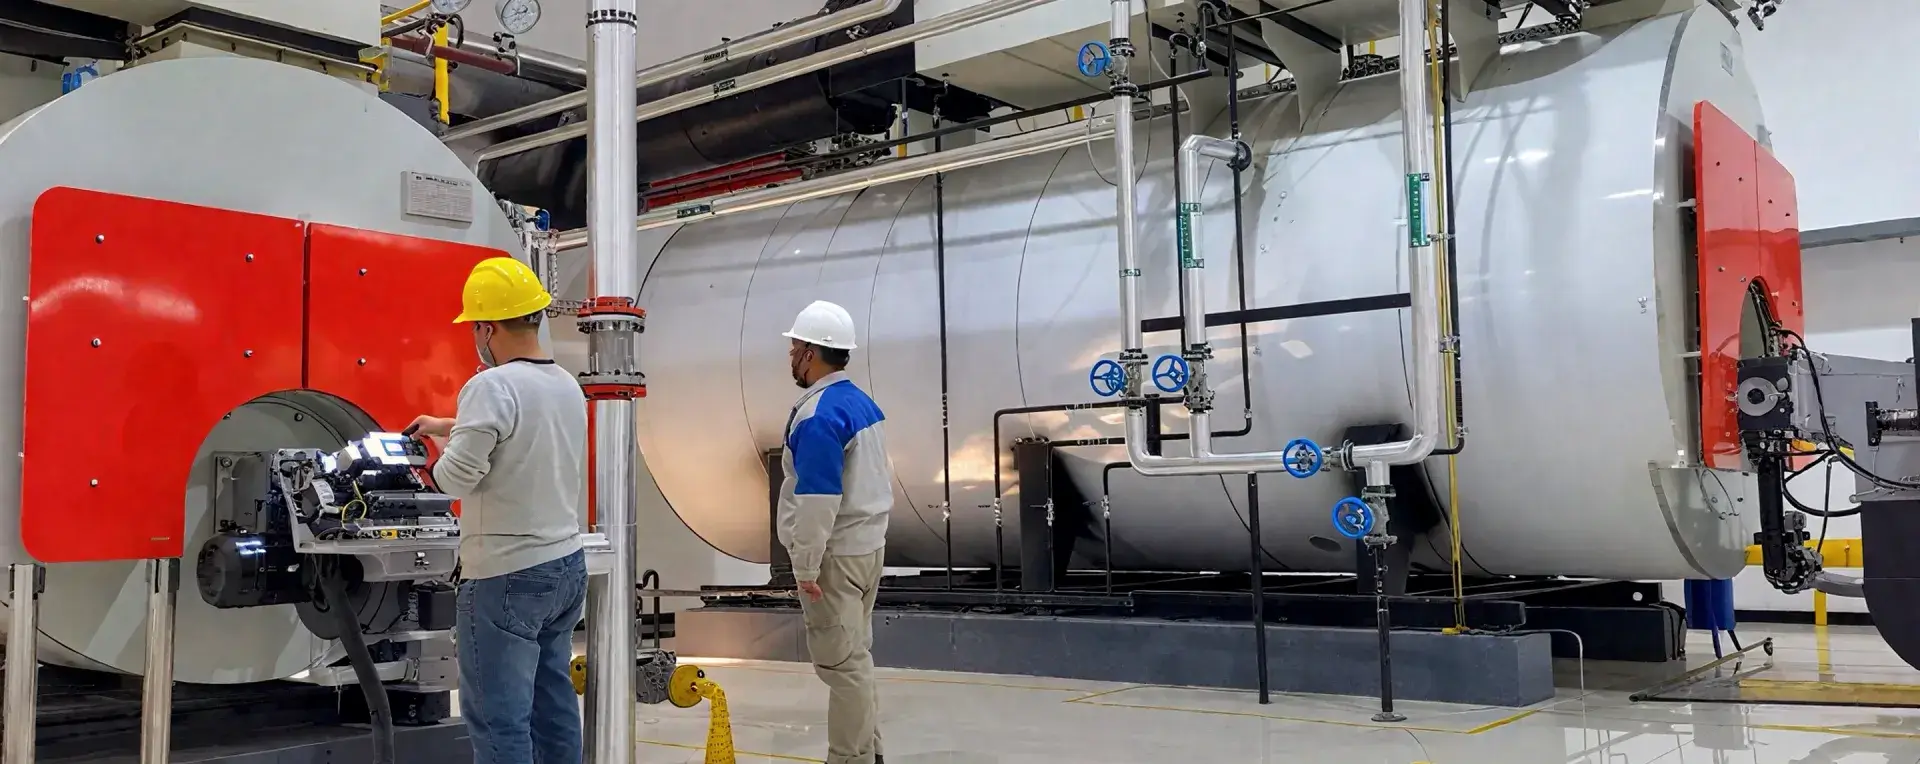
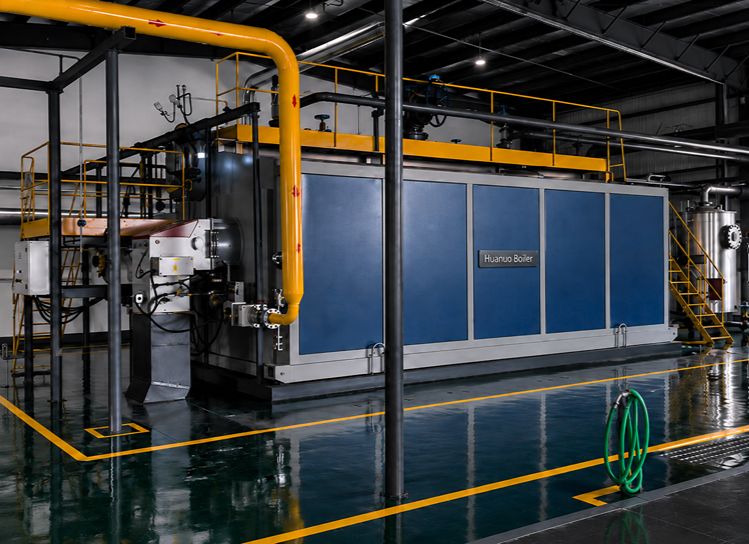
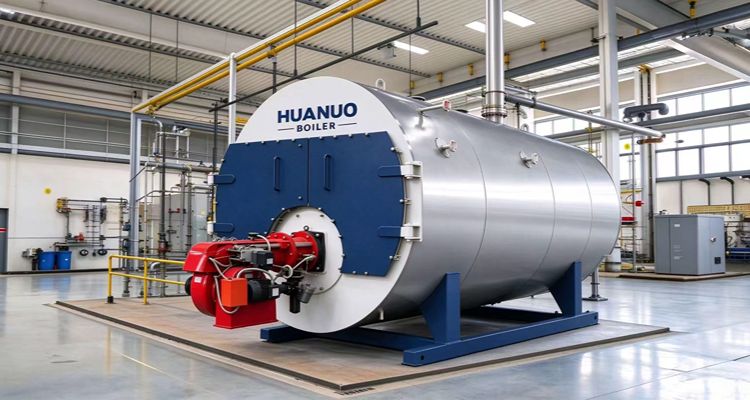
Given the characteristics of chemical production—which involves continuous operations, stable steam loads, and extremely high standards for quality and safety—Huanuo Boilers equipped the client with an SZS15-1.6-Q integrated condensing gas-fired steam boiler:
Request a Solution
The boiler features a dual-drum, longitudinally arranged large-firebox design that optimizes the layout of radiation and convection heat transfer surfaces. Combined with a high-efficiency condensation recovery unit at the rear, it fully recovers waste heat from flue gases, achieving a comprehensive thermal efficiency exceeding 98%. Compared to traditional gas boilers, fuel consumption is reduced by more than 15%, resulting in significant energy savings.
Equipped with a fully automatic low-NOx burner and flue gas recirculation technology, NOx emissions are well below the limits set by Indonesia’s current environmental regulations. This easily meets increasingly stringent emission inspections and helps enterprises achieve low-carbon manufacturing.
Leveraging Huano Boilers’ extensive engineering experience in the chemical industry, the equipment consistently delivers high-quality steam with sufficient dryness and stable pressure, fully meeting the heat source requirements for core processes such as chemical reactions and distillation, thereby ensuring the intrinsic safety of continuous production from the source.
The boiler control system supports fully automated operation, adaptive load regulation, and multi-level safety interlock protection. Local Indonesian operators can master the system after a short training period, significantly reducing labor costs and operational workload.
Core Project Advantages
Steam energy consumption per unit of product has dropped significantly, resulting in an average annual natural gas cost savings of approximately 15% and a shorter-than-expected return on investment.
The boiler’s emission indicators passed local environmental inspections on the first attempt, earning the company a reputation for green production and enabling it to successfully enter the green supply chains of multiple international clients.
Steady steam pressure and consistent quality effectively prevent batch non-conformities caused by fluctuations in the heat source, thereby improving overall product yield.
Since the equipment was commissioned, there have been zero unplanned shutdowns, providing a solid guarantee for the long-term safe operation of chemical plants.
Client Testimonial

Hendra Setiawan.
Director of Engineering and Technology

Budi Santoso.
Equipment Manager, a major paper group in Indonesia

María González.
Production Director, a pharmaceutical company in Mexico

Ahmed Hassan.
Head of Engineering, a hotel group in Egypt

Mehmet Yılmaz
Production Manager, a textile dyeing and finishing company in Türkiye

Rafiq Islam.
Operations Supervisor, a garment washing company in Bangladesh

Khalid Al-Farsi
Plant Manager, a food processing plant in Saudi Arabia

Johan van der Merwe
Energy Manager, a beverage producer in South Africa

Rajesh Kumar
Technical Director, a chemical company in India

Dmitry Ivanov
Operations Manager, a district heating company in Russia

Camila Rojas.
Production Head, a fruit and vegetable processor in Chile